Choosing a Cnc Centre Lathe in 2026 is a production decision, not a showroom decision. The right machine must match your materials, tolerances, batch sizes, and operator skills. A polished brochure cannot reveal every limitation.
Mike Lynch, a respected CNC programming educator and author, once stated, “A CNC machine is only as good as the program, tooling, and setup behind it.” That principle remains practical. A powerful spindle cannot compensate for poor workholding. High rapid speed means little when chip control is weak. Check the machine cutting real steel, not only turning an impressive aluminum sample.
This guide examines spindle power, chuck capacity, swing diameter, bed length, turret performance, control systems, and thermal stability. It also considers service response, spare-part access, software compatibility, and training. These details often decide whether a lathe earns money or waits beside the workshop wall.
Look closely.
A reliable Cnc Centre Lathe should produce consistent parts during long cycles, with measurable repeatability and manageable maintenance. Ask suppliers for test-cut data, inspection records, warranty terms, and references from similar factories. Standards and independent verification matter, but they do not replace practical trials.
There is no universally best model. That is the uncomfortable part. A smaller machine may outperform a larger one when floor space, energy use, and job mix matter. Buyers can also overestimate future capacity and pay for unused features. This guide helps you question those assumptions before signing a purchase order.
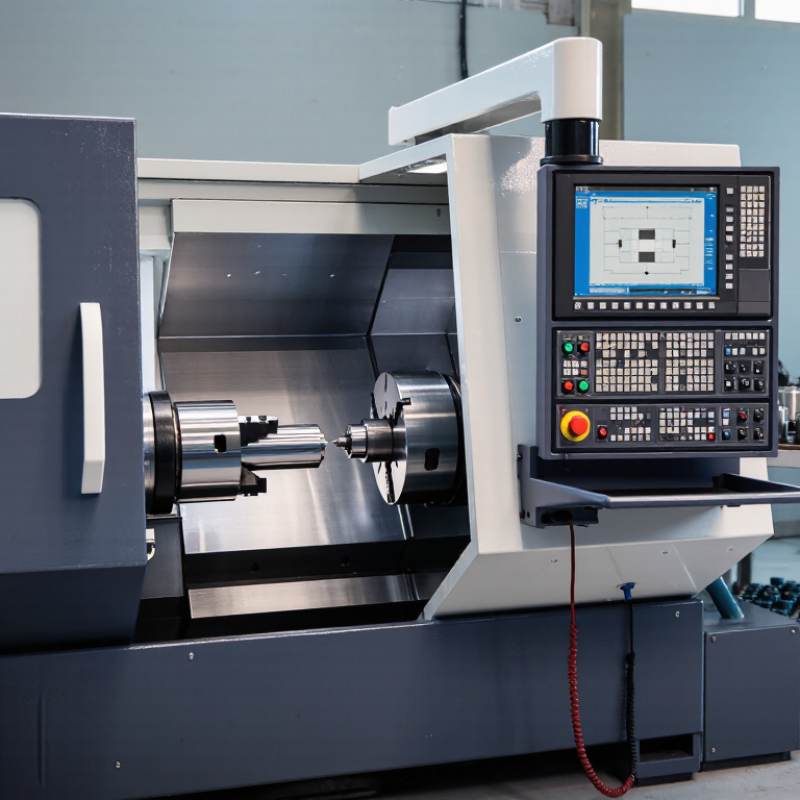
Choosing a CNC centre lathe in 2026 starts with its working envelope, not its catalogue price. A two-axis flat-bed lathe suits general shaft and bush machining. A slant-bed turning centre usually offers better chip flow and stronger production access. Live tooling and a C-axis add milling operations, but they also increase setup complexity.
Check swing over bed, maximum turning diameter, turning length, spindle bore, and chuck size. A machine with 500 mm swing may still accept only a smaller practical workpiece. Measure the part, chuck, toolholder, and tailstock clearance together. Spindle speed matters too. High speed helps small aluminium parts, while high torque supports larger steel components. Bigger is not always better.
ISO 230-2 evaluates axis positioning accuracy and repeatability under defined test conditions. It commonly reports unidirectional and bidirectional results, including systematic deviation and scatter. These results are not universal “accuracy classes” for every lathe. Buyers should request the actual test report, test temperature, axis travel, and compensation status. A quoted ±0.005 mm may describe positioning, not finished part accuracy. Tool wear, thermal growth, chuck condition, and programming still influence the cut. I have seen excellent reports produce disappointing parts after long warm-up cycles.
Look for acceptance data that matches your production axis and travel. Run a sample test when possible. The report is evidence, not a promise.
The specifications below are practical purchasing reference ranges. ISO 230-2 defines test methods and measurement terms for positioning accuracy and repeatability; it does not establish universal machine accuracy classes. Actual performance depends on machine configuration, thermal conditions, tooling, workholding, material, and measurement method.
| CNC Centre Lathe Type | Typical Workpiece | Typical Swing Over Bed | Typical Turning Diameter | Typical Turning Length | Common Features | Best Application |
|---|---|---|---|---|---|---|
| 2-axis CNC centre lathe | General shaft, bush, thread, and facing work | 350–800 mm | 200–500 mm | 300–1,500 mm | X and Z axes, chuck, tailstock, turret or gang tooling | Low- to medium-volume general production |
| Slant-bed CNC lathe | Short and medium-length turned components | 400–900 mm | 250–650 mm | 300–1,250 mm | Rigid slant bed, improved chip flow, automatic tool turret | Efficient batch and production machining |
| Long-bed CNC centre lathe | Long shafts, rollers, spindles, and pipe components | 600–1,400 mm | 350–900 mm | 1,500–6,000 mm | Extended bed, steady rest, follow rest, large tailstock | Large-diameter or long slender workpieces |
| Turn-mill centre | Complex parts requiring turning and milling in one setup | 500–1,000 mm | 250–700 mm | 400–1,500 mm | Live tooling, C-axis, optional Y-axis, driven tools | Reduced setups and higher process integration |
| Swiss-type CNC lathe | Small, slender, and precision bar-fed components | Not usually specified by conventional bed swing | 3–32 mm bar capacity is common | 30–300 mm typical part length | Guide bushing, sliding headstock, gang tools, sub-spindle | Medical, electronics, and miniature precision parts |
| Heavy-duty CNC centre lathe | Large forgings, flanges, rolls, and heavy shafts | 900–2,500 mm | 700–2,000 mm | 1,000–8,000 mm | High torque, large spindle bore, steady rests, reinforced structure | Heavy metal removal and large-part machining |
| Size Group | Typical Chuck Diameter | Typical Spindle Bore | Typical Motor Power | Typical Maximum Workpiece Mass | Recommended Use |
|---|---|---|---|---|---|
| Compact | 100–200 mm | 20–52 mm | 5.5–15 kW | 50–300 kg | Small parts, limited floor space, short-cycle work |
| Medium | 200–315 mm | 52–80 mm | 11–30 kW | 300–1,000 kg | General production and mixed component sizes |
| Large | 315–800 mm | 80–160 mm | 22–75 kW | 1,000–5,000 kg | Large shafts, flanges, and high-volume chip removal |
| Extra-large | 800–2,000 mm or larger | 160–500 mm or larger | 45–150 kW | 5,000–50,000 kg | Heavy engineering and oversized workpieces |
| Practical Accuracy Band | Typical Bidirectional Positioning Accuracy Target* | Typical Bidirectional Repeatability Target* | Suitable Work | Buyer Verification Point |
|---|---|---|---|---|
| Standard production | Up to approximately 0.030 mm per 1,000 mm axis travel | Up to approximately 0.012 mm | General turning, roughing, and routine batch work | Request the complete ISO 230-2 test report, not only a brochure value |
| Precision production | Up to approximately 0.020 mm per 1,000 mm axis travel | Up to approximately 0.008 mm | Close-tolerance shafts, bearing seats, and repeat batches | Check test temperature, axis travel, sampling points, and compensation status |
| High-precision production | Up to approximately 0.012 mm per 1,000 mm axis travel | Up to approximately 0.005 mm | Precision components and demanding finishing operations | Confirm thermal stabilization, machine foundation, alignment, and calibration traceability |
| Ultra-precision application | Below approximately 0.010 mm per 1,000 mm axis travel | Below approximately 0.003 mm | Specialized precision work under controlled conditions | Use an independent acceptance test and define environmental limits in the contract |
*The accuracy bands above are purchasing guidelines, not ISO-defined classes. ISO 230-2 test results should identify the measured axis, travel length, positioning direction, repeatability, reversal behavior, measurement uncertainty, environmental conditions, and whether error compensation was active.
| Buying Dimension | Recommended Check | Why It Matters |
|---|---|---|
| Work envelope | Select at least 10–20% more turning diameter and length than the largest regular part | Allows clearance for jaws, tools, tailstock, steady rests, and safe chip evacuation |
| Spindle and bar capacity | Match spindle bore and chuck capacity to the largest bar, chucking diameter, and workholding method | Prevents workholding restrictions and unnecessary remounting |
| Power and torque | Compare continuous power, peak power, torque curve, and rated spindle speed | Motor power alone does not show low-speed heavy-cutting capability |
| Tooling system | Check turret station count, tool size, live-tool speed, Y-axis travel, and tool-change time | Determines setup flexibility and cycle-time efficiency |
| Accuracy acceptance | Specify ISO 230-2 measurement conditions and acceptance limits before delivery | Creates an objective basis for machine acceptance and future recalibration |
| Thermal control | Evaluate spindle warm-up, coolant temperature control, axis compensation, and shop temperature stability | Thermal drift can affect dimensional accuracy during long production runs |
| Installation requirements | Confirm footprint, floor loading, electrical supply, compressed air, coolant, extraction, and lifting access | A suitable machine can still fail to meet production needs if site services are inadequate |