China’s flexible packaging industry has become a serious source of solvent-free equipment. This guide examines China’s top 10 Solvent Free Lamination machine manufacturers. It focuses on practical performance, not attractive brochures alone.
A capable machine should control adhesive coating weight, web tension, nip pressure, and curing conditions. These details affect bond strength, curl, wrinkles, and production waste. Some lines handle films, aluminium foil, paper, and metallised substrates. Others perform better with narrower webs or specific adhesive systems. Factory trials matter.
Antonio Sada, president of Nordmeccanica, has often described the industry’s direction simply: “Solventless is the future of laminating.” His view reflects a clear manufacturing shift. Solvent-free systems can reduce solvent handling, drying energy, and workplace emissions when properly installed and operated. However, the process is not automatically perfect. Incorrect adhesive temperature or uneven coating can create bubbles, weak bonds, and expensive downtime.
That is the difficult part.
This overview compares manufacturers through engineering experience, machine configuration, automation, after-sales support, and documented customer use. It also considers working width, maximum speed, adhesive technology, inspection options, and operator training. Public information is sometimes incomplete, so no ranking should be treated as permanent. A machine that performs well on snack-film structures may not suit pharmaceutical foil or heavy paper laminates.
Readers should request sample trials, technical drawings, reference contacts, and total operating costs. The lowest purchase price may hide slower commissioning or limited service coverage. Reliable selection requires evidence from the finished laminate, not promises made during a sales meeting.
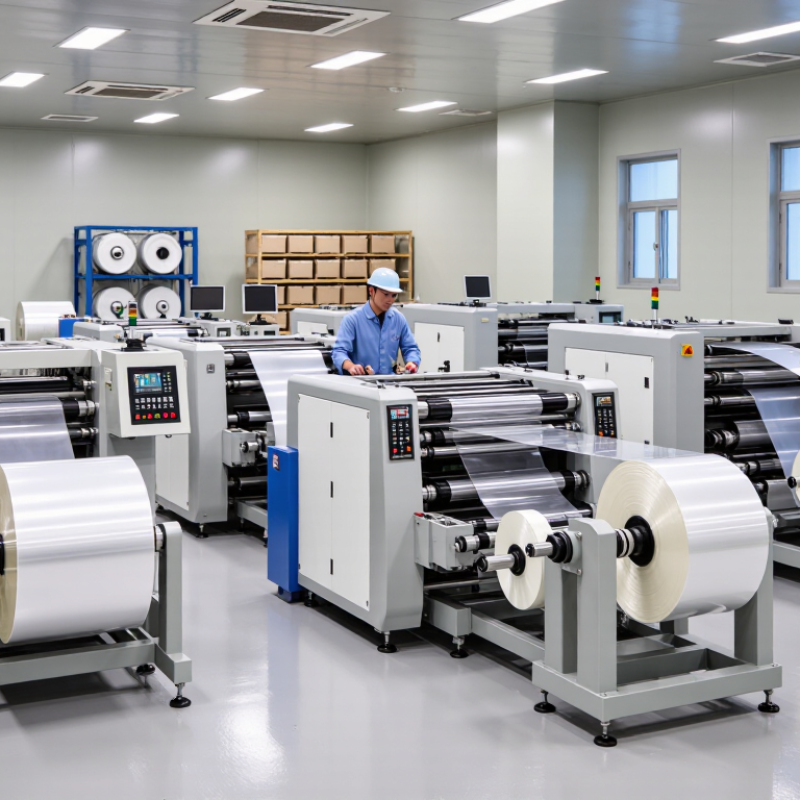
China’s top ten solvent-free lamination machine manufacturers are increasingly judged by one practical figure: line speed. In the 300–600 m/min range, speed is not a marketing ornament. It affects coating stability, web tension, curing time, and waste control. Experienced converters know that a machine reaching 600 m/min in a trial may run closer to 420 m/min during everyday production. Real conditions matter. Film thickness, adhesive temperature, and substrate stiffness can change the result.
At 300–400 m/min, operators often gain a wider process window and easier setup. This range suits many flexible packaging jobs, especially when graphics, film gauge, or humidity varies. Above 450 m/min, small errors become visible quickly. A slight tension imbalance can create wrinkles, telescoping rolls, or uneven bonding. Good equipment should provide responsive tension control, accurate metering, automatic splice handling, and clear data logs. Safety guarding and maintenance access also deserve serious attention.
A credible supplier should demonstrate stable production, not only peak speed. Ask for test results using comparable films, adhesive grades, coating weights, and roll widths. Inspect bond strength, residual odor, energy use, and changeover time. Visit a working installation when possible. It is easy to underestimate training. Even advanced automation cannot correct poor parameter choices. The uncomfortable truth is that the fastest line is not always the most profitable one. Uptime, repeatability, and controlled waste usually decide the investment.
China Top 10 Solvent Free Lamination Machine Manufacturers?
When comparing solvent-free lamination machine manufacturers in China, output should mean more than maximum line speed. Check stable running speed, usable web width, roll diameter, and changeover time. A machine rated at 400 meters per minute may perform differently with thin film, paper, or aluminum foil. Ask for trial data using your actual materials. My experience is that realistic output matters more than impressive brochure figures. Data can still mislead.
Coating weight control directly affects bond strength, cost, and appearance. Look for precise metering systems, automatic gap adjustment, and clear weight feedback. Request coating results at low, medium, and high settings. Small variations can create wrinkles or weak edges. VOC control also needs careful review. Solvent-free systems reduce solvent use, but curing, adhesive odor, exhaust design, and cleaning procedures still deserve attention. A good supplier should explain these details without vague promises.
Tips: Inspect sample rolls under light. Measure coating weight across the web, not only at the center. Review factory acceptance records, maintenance access, and operator training. Certifications such as ISO 9001, CE, or region-specific documents should match the delivered machine. Verify certificate scope and validity. Do not accept copied files. One overlooked detail can delay production. A perfect test is rare, so record every limitation before purchasing.
| Rank | Anonymous Manufacturer Profile | Maximum Web Width (mm) | Designed Line Speed (m/min) | Typical Adhesive Coating Weight (g/m²) | Coating Weight Tolerance | VOC-Control Characteristics | Typical Application Range | Certification or Compliance Evidence to Request |
|---|---|---|---|---|---|---|---|---|
| 1 | Profile A — High-output flexible-packaging platform | 1,300 | 400–500 | 1.0–2.5 | Typically ±0.10 g/m² | Solvent-free adhesive system; enclosed metering section; no intentional solvent emissions from the adhesive process. | PET, BOPP, CPP, PE, aluminum foil, paper, and multilayer packaging films. | CE-related technical file, electrical safety documentation, ISO 9001 evidence, and machine risk assessment. |
| 2 | Profile B — Wide-web industrial laminator | 1,600 | 300–450 | 1.2–3.0 | Typically ±0.12 g/m² | 100% solids adhesive process; heated adhesive supply; closed circulation to reduce operator exposure and material waste. | Large-format packaging, technical films, foil laminates, and hygienic-material structures. | CE conformity documentation, ISO 9001 certificate, electrical component declarations, and factory acceptance test records. |
| 3 | Profile C — Precision coating and laminating system | 1,300 | 250–400 | 0.8–2.2 | Typically ±0.08 g/m² | Closed gravimetric or precision pump control; solvent-free adhesive formulation; VOC levels depend on incoming substrates and inks. | High-barrier films, retort structures, pharmaceutical packaging, and thin-gauge webs. | ISO 9001 evidence, calibration certificates for weighing systems, CE documentation, and documented coating uniformity results. |
| 4 | Profile D — Medium-speed packaging laminator | 1,050 | 250–350 | 1.5–3.5 | Typically ±0.15 g/m² | Solvent-free coating head with temperature-controlled adhesive delivery; no drying oven required for the adhesive layer. | General food packaging, labels, sachets, and standard film-to-film laminations. | CE-related documents, ISO 9001 evidence, food-contact material compatibility documentation where applicable, and FAT protocol. |
| 5 | Profile E — Compact high-efficiency laminator | 1,000 | 200–300 | 1.0–3.0 | Typically ±0.15 g/m² | Low-inventory adhesive circuit, automatic temperature monitoring, and solvent-free operation with reduced energy demand. | Short and medium production runs, flexible packaging, paper-film combinations, and specialty laminates. | ISO 9001 evidence, electrical safety test reports, CE technical documentation, and operator-safety validation. |
| 6 | Profile F — Foil and barrier-film specialist platform | 1,300 | 220–350 | 1.5–3.5 | Typically ±0.15 g/m² | Heated adhesive and nip-temperature control; solvent-free process supports low VOC emissions from the machine itself. | Aluminum foil, metallized films, high-barrier packaging, and chemical-resistant structures. | CE documentation, ISO 9001 evidence, pressure and temperature calibration records, and material compatibility test reports. |
| 7 | Profile G — Paper, film, and nonwoven laminator | 1,200 | 180–300 | 2.0–4.0 | Typically ±0.20 g/m² | Solvent-free adhesive application with controlled web tension and enclosed heated reservoirs for stable processing. | Paper packaging, nonwoven materials, release liners, and absorbent-product components. | ISO 9001 evidence, CE-related machine documentation, web-tension calibration records, and applicable product-safety declarations. |
| 8 | Profile H — Flexible modular laminating line | 1,300 | 200–320 | 1.0–3.5 | Typically ±0.15 g/m² | Modular solvent-free coating unit, automatic adhesive temperature control, and reduced exhaust requirements compared with solvent-based lines. | Mixed-substrate packaging, decorative films, labels, and customized production configurations. | CE technical file, ISO 9001 evidence, PLC and electrical conformity documents, and line-integration risk assessment. |
| 9 | Profile I — Entry-to-mid-range solvent-free laminator | 1,000 | 150–250 | 1.5–4.0 | Typically ±0.20 g/m² | Basic enclosed adhesive system; no intentional solvent addition; ventilation requirements remain dependent on inks, primers, and substrate materials. | Standard flexible packaging, sampling, pilot production, and lower-volume converting. | CE-related documentation, ISO 9001 evidence, electrical safety testing, and documented trial-lamination results. |
| 10 | Profile J — Customized specialty-film laminator | 1,300 | 180–300 | 0.8–3.0 | Typically ±0.10–0.20 g/m² | Application-specific solvent-free coating head, recipe control, and minimized VOC contribution from adhesive application. | Medical-packaging films, electronics materials, specialty labels, and engineered multilayer webs. | CE documentation, ISO 9001 evidence, process validation records, calibration certificates, and customer-specific compliance documents. |
China’s top 10 solvent-free lamination machine manufacturers are increasingly judged by technology, production capacity, and export reach. Their equipment typically combines two-component adhesive dosing, automatic tension control, and precision coating systems. These features support thinner films, stable bonding, and lower energy use.
Technology matters most.
Industry research from Smithers, including The Future of Flexible Packaging to 2028, identifies sustainability and material efficiency as major packaging priorities. Solvent-free lamination responds to both demands.
Several leading Chinese manufacturers now offer line speeds above 400 meters per minute, while advanced models can exceed 600 meters per minute under suitable material conditions. However, advertised speed is not final proof. Adhesive curing, film width, and operator skill can change real output.
Capacity separates established suppliers from smaller workshops. The strongest manufacturers operate large assembly facilities, maintain testing laboratories, and provide machines for film, foil, and paper structures.
Export reach is another key measure. According to UN Comtrade data, China remains a major exporter of packaging machinery, serving converters across Southeast Asia, the Middle East, Europe, and Latin America. Service networks, spare-parts response, and commissioning experience often matter more than catalog claims.
The ranking still has limits. Public data is uneven, and some capacity figures are self-reported. A reliable buyer should inspect factory tests, energy records, adhesive waste, and installed references before choosing among the ten.
Numbers can look impressive. Production evidence is better.
Comparing the China top 10 solvent-free lamination machine manufacturers requires more than checking maximum speed. The key test is stable adhesive coating between 0.8 and 2.5 g/m². At the lower setting, small metering errors can create weak bonds or dry edges. At the higher setting, excess adhesive may increase curing time and waste. A practical comparison should include measured coating samples, not only catalog figures.
Substrate range also changes machine value. Flexible film, aluminum foil, paper, and metallized structures need different tension control and nip pressure. A machine handling 12-micron film may not run thick paper smoothly. Ask suppliers for trial records using your actual width, thickness, and surface treatment. Watch the web near the coating head. Wrinkles often reveal problems before the final laminate does.
Experienced operators also inspect temperature stability, pump response, mixing accuracy, and cleaning access. These details affect daily reliability. A useful trial should record coating weight, bond strength, line speed, and curing results after 24 and 72 hours. Numbers matter.
Some comparisons remain imperfect. Laboratory samples may look excellent, while long production runs expose edge buildup or uneven tension. Therefore, procurement teams should challenge test conditions and repeat critical trials. A broad substrate list is only a starting point. The better machine is the one that holds 0.8–2.5 g/m² consistently across real materials and changing production demands.
When comparing China’s top solvent-free lamination machine manufacturers, examine the complete line, not only the laminator. A practical configuration includes adhesive dosing, mixing, coating, unwinding, rewinding, tension control, and curing space. Automatic viscosity monitoring can reduce coating variation. However, sensors cannot replace trained operators.
Energy use is often lower because solvent-free systems avoid large drying ovens and exhaust treatment. The European Commission’s Best Available Techniques guidance identifies solvent control and heat recovery as major efficiency factors in coating operations. The Flexible Packaging Association also reports that flexible packaging can use about 60% less plastic than comparable rigid formats. That advantage depends on stable coating weight and low scrap. A poorly tuned line wastes materials quickly.
Maintenance planning should cover pumps, filters, mixing heads, web guides, and temperature controls. Ask for cleaning intervals, spare-part availability, and documented service response times. Smithers’ flexible packaging market reports show continued demand for high-performance barrier structures, increasing pressure on uptime and quality consistency. For ROI, calculate output per hour, adhesive consumption, labor, rejected rolls, electricity, and curing inventory. Use real production records, not optimistic quotations. A spreadsheet can look convincing and still be wrong. Payback may change sharply when a line runs shorter jobs, thicker films, or frequent product changes. Test samples under actual humidity and speed conditions before approving the final configuration.

Since 1984, Thermostop has been a reputable manufacturer of Industrial Sectional Doors, Cold Storage Doors and Specialty Doors such as Impactable Breakaway doors, Acoustic Doors and Ballistic Doors.
Contact