Choosing the right Metal Polishing Machine can shape surface quality, production speed, labor costs, and long-term maintenance. Global buyers face a crowded market. Different machines suit stainless steel sheets, aluminum parts, tubes, fittings, cookware, and precision components. A belt polishing machine may handle broad flat surfaces efficiently. A tube polisher can create a consistent finish around curved edges. Vibratory, barrel, disc, wheel, brush, planetary, CNC, and automatic polishing systems serve different production needs.
This guide examines ten widely used machine types through practical purchasing criteria. These include abrasive compatibility, workpiece size, polishing speed, automation level, dust control, operator safety, spare-part access, and finished-surface consistency. A bright mirror finish needs different control than a brushed No. 4 finish. Small workshops may value flexible adjustment. Large factories may prioritize cycle time and repeatability. Details matter.
Real production conditions can be less predictable.
Material hardness, part geometry, and operator skill often change the result. Supplier claims should therefore be checked against samples, technical drawings, test reports, and after-sales support. Buyers should also confirm voltage, installation requirements, maintenance intervals, and applicable workplace safety standards. No machine is perfect for every application. That is worth remembering. This overview combines industry knowledge with practical evaluation, while recognizing that local requirements and production goals vary. Its purpose is to help engineers, distributors, and purchasing teams compare suitable options with greater confidence.
Metal Polishing Machines: Purpose, Working Principles, and Main Categories
Metal polishing machines remove scratches, burrs, oxidation, and uneven surface marks. They also create controlled gloss before plating, painting, or final inspection. Their core action combines pressure, abrasive movement, and relative speed. A rotating wheel, abrasive belt, or media bed contacts the workpiece repeatedly. Heat and friction then reshape the surface at a microscopic level. The target matters. A mirror finish is not always better. According to Grand View Research’s Metal Finishing Market report, the global market was valued at roughly USD 100 billion in 2022, with steady growth forecast through 2030. That expansion reflects wider demand for repeatable surface quality in automotive, aerospace, medical, and general fabrication.
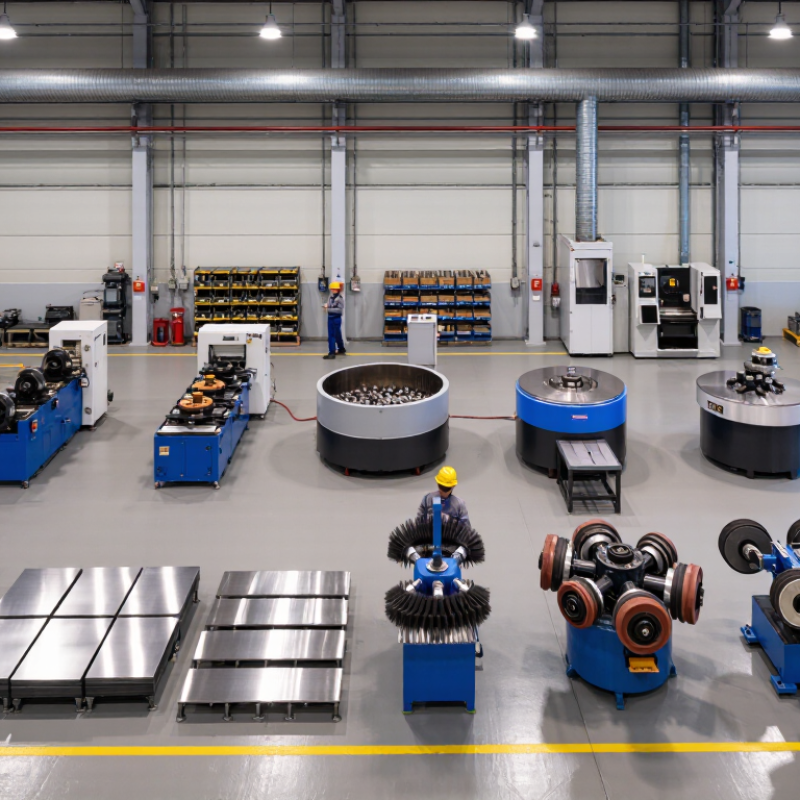
Main categories include belt polishers, buffing-wheel machines, vibratory finishers, barrel machines, centerless polishers, and robotic systems. Belt machines suit flat panels and welded frames. Wheel polishers handle visible decorative surfaces. Vibratory and barrel systems process many small parts together, although they can leave media marks on delicate edges. Centerless machines support continuous cylindrical production. Robotic cells offer consistent pressure and programmed paths, but setup costs remain significant. ASTM and ISO surface-texture practices remind buyers to specify measurable roughness, not only visual shine. One selection mistake can reduce throughput. Operators should test the actual alloy, geometry, abrasive grade, cycle time, and cooling method before purchase. Practical trials often reveal problems that brochures hide.
| No. | Machine Type | Primary Purpose | Working Principle | Typical Process | Suitable Metals | Common Applications | Key Advantages | Main Limitations |
|---|---|---|---|---|---|---|---|---|
| 1 | Belt Polishing Machine | Fast removal of weld seams, burrs, scale, scratches, and surface irregularities. | An abrasive belt runs over contact wheels or platens and removes material through controlled friction against the workpiece. | Grinding, deburring, satin finishing, blending, and pre-polishing. | Stainless steel, carbon steel, aluminum, brass, copper, and titanium. | Sheet metal, tubes, welded frames, cookware, hardware, and fabricated parts. | High stock-removal rate, flexible abrasive selection, and suitable for flat or contoured surfaces. | Abrasive belts wear over time; operators must control pressure to avoid uneven edges or overheating. |
| 2 | Centerless Polishing Machine | Continuous polishing of cylindrical parts without using a conventional chuck or center support. | A regulating wheel controls rotation and feed while an abrasive wheel contacts the workpiece against a work-rest blade. | Through-feed or plunge polishing, grinding, and fine finishing. | Stainless steel, hardened steel, brass, copper, aluminum, and nickel alloys. | Rods, shafts, pins, tubes, rollers, and other rotationally symmetrical components. | High throughput, consistent roundness, and efficient processing of long cylindrical parts. | Primarily designed for round parts; setup and wheel alignment require skilled adjustment. |
| 3 | Disc Polishing Machine | Polishing flat surfaces, edges, and small components with a rotating abrasive or polishing disc. | A horizontal or vertical disc rotates at controlled speed while the workpiece is pressed against an abrasive or compound-coated surface. | Deburring, edge rounding, surface smoothing, and bright polishing. | Aluminum, stainless steel, brass, copper, steel, and zinc alloys. | Small plates, fittings, sheet edges, hardware, cutlery, and precision components. | Compact design, quick abrasive changes, and good control for localized finishing. | Contact pressure must be controlled carefully; large or irregular parts may be difficult to fixture. |
| 4 | Rotary Barrel Tumbling Machine | Batch deburring, edge softening, cleaning, and general finishing of numerous small parts. | Parts, abrasive media, water, and compounds rotate inside a barrel, producing repeated sliding and impact contact. | Mass finishing, deburring, burnishing, descaling, and cleaning. | Steel, stainless steel, aluminum, brass, copper, zinc, and die-cast alloys. | Fasteners, castings, stamped parts, gears, fittings, and small machined components. | Processes many small parts at once and reduces manual deburring labor. | Parts may contact one another; not ideal for delicate, flat, or highly cosmetic components. |
| 5 | Vibratory Finishing Machine | Mass finishing with improved access to recesses, internal edges, and complex part profiles. | A vibratory bowl or tub oscillates at controlled frequency, causing media and workpieces to rub against each other. | Deburring, polishing, burnishing, radiusing, and oxide removal. | Steel, stainless steel, aluminum, brass, copper, titanium, and zinc alloys. | Precision castings, automotive parts, medical components, fittings, and stamped products. | Good batch consistency, broad media choices, and better treatment of complex geometries than simple barrels. | Processing can take several hours; media separation and wastewater management may be required. |
| 6 | Centrifugal Disc Finishing Machine | Accelerated deburring and polishing for small and medium-sized precision parts. | A rotating disc creates a high-energy toroidal flow of media, compound, and workpieces inside the processing chamber. | Fine deburring, edge rounding, burnishing, and high-speed surface finishing. | Steel, stainless steel, aluminum, brass, copper, and titanium alloys. | Precision machined parts, small gears, connectors, implants, and intricate hardware. | Much faster than conventional vibratory finishing and effective on small complex components. | Higher impact energy can damage fragile parts; batch capacity is generally limited by chamber size. |
| 7 | Electropolishing System | Produces a smooth, clean, and bright metallic surface while removing a controlled microscopic layer. | The workpiece acts as the anode in an electrolytic cell; direct current dissolves surface metal into an electrolyte bath. | Electrochemical smoothing, micro-deburring, brightening, and passivation-supporting surface treatment. | Stainless steel, nickel alloys, cobalt-chromium, copper, and selected aluminum alloys. | Pharmaceutical equipment, food-processing components, laboratory parts, medical devices, and precision tubing. | Improves cleanability and corrosion resistance while reaching some complex internal surfaces. | Requires chemical handling, ventilation, wastewater treatment, and material-specific process control. |
| 8 | Magnetic Abrasive Finishing Machine | Fine finishing and deburring of small parts, narrow channels, holes, and hard-to-reach areas. | A rotating magnetic field moves ferromagnetic abrasive pins through gaps and along the workpiece surface. | Micro-deburring, edge smoothing, polishing, and internal passage finishing. | Steel, stainless steel, brass, copper, aluminum, and non-ferrous precision parts. | Jewelry components, precision fittings, watch parts, small machined parts, and medical components. | Reaches small holes and narrow spaces with short cycle times and minimal fixture requirements. | Limited for large workpieces or heavy stock removal; magnetic-field settings must match part geometry. |
| 9 | Robotic Polishing Cell | Automated and repeatable polishing of large, heavy, or geometrically complex components. | A programmed industrial robot controls tool path, contact force, speed, and orientation using abrasive belts, wheels, or brushes. | Grinding, weld blending, satin finishing, mirror polishing, and multi-stage finishing. | Stainless steel, aluminum, carbon steel, brass, copper, and nickel alloys. | Automotive components, sanitary vessels, large fittings, cookware, furniture parts, and fabricated structures. | Consistent results, reduced operator exposure to dust and vibration, and flexible multi-axis movement. | Higher initial investment; programming, tooling, fixturing, and process integration require technical expertise. |
| 10 | CNC Polishing and Superfinishing Machine | Precision finishing where surface roughness, geometry, and repeatability must be tightly controlled. | Computer-controlled axes guide abrasive tools or polishing heads along programmed paths while controlling feed, pressure, and speed. | Fine grinding, lapping, polishing, superfinishing, and dimensional correction. | Hardened steel, stainless steel, carbide, ceramics, nickel alloys, aluminum, and titanium. | Bearings, hydraulic parts, precision shafts, molds, aerospace components, and high-tolerance tooling. | High repeatability, programmable process parameters, and excellent control of surface texture and form. | Higher purchase and maintenance costs; economical mainly for precision work or medium-to-high production volumes. |